A useful CRGO purchasing checklist covers seven items: the grade and the standard it is ordered to, nominal thickness, width and coil format, guaranteed core loss at a stated test condition, insulation coating, any processing such as slitting or cutting, and the inspection documents you need at delivery. If an enquiry fixes all seven, suppliers can quote like for like and the material that arrives can be checked against what was ordered. If any one is missing, quotes drift apart and disputes start at incoming inspection.
This guide is written for transformer core makers and lamination shops buying cold-rolled grain-oriented (CRGO) electrical steel. It explains what each line of the enquiry means, where buyers usually lose time, and ends with a template you can copy into your next RFQ.
Start with the form of material you are buying
Many CRGO enquiries go wrong before any grade is named, because buyer and supplier picture a different product. Raw material, processed laminations, an assembled core and a finished transformer are four different purchases with different specifications, test methods and responsibilities. Say which one you want in the first line.
| Form | What it is | What the enquiry must define |
|---|---|---|
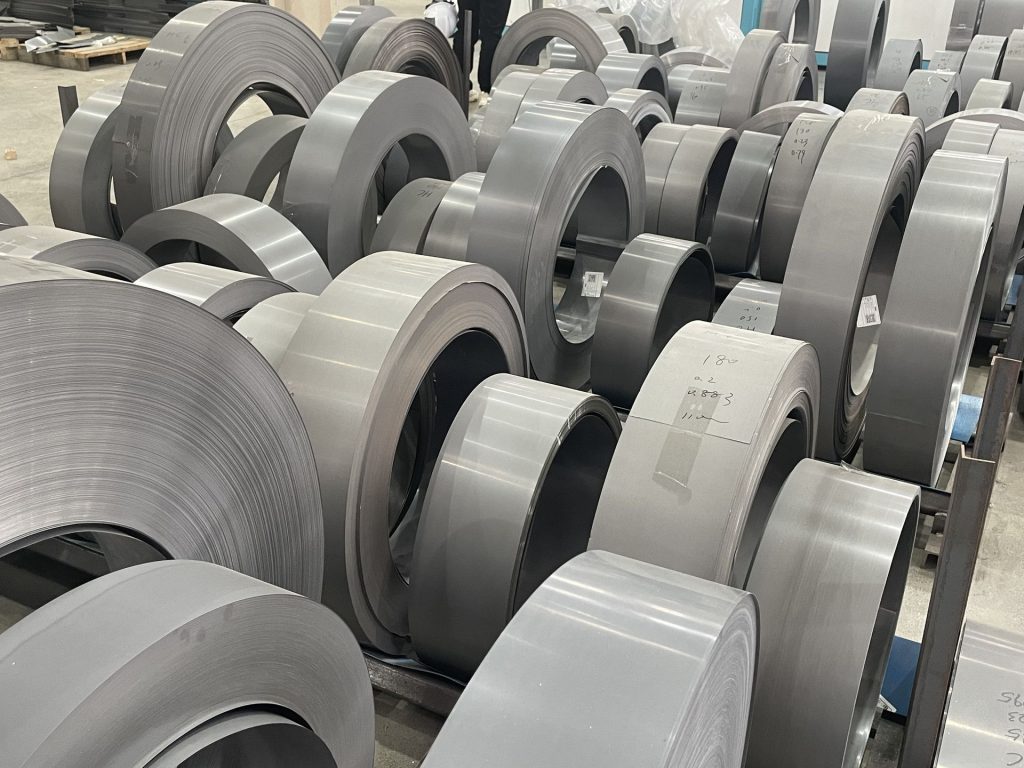
| Master coil | Full-width coil as produced by the mill | Grade, standard, thickness, width, coating, coil ID/OD and weight range, documents |
| Slit coil | Master coil slit to the widths of your core steps | All of the above plus slit widths, width tolerance, burr limit, camber, edge condition |
| Cut laminations | Strip cut to length and joint angle (for example step-lap) | Drawing, lengths, angles, holes, burr limit, stacking and packing, whether stress-relief annealing is done |
| Assembled core | Laminations stacked and clamped into a core | Core drawing, stacking method, mass, test requirements agreed with the transformer designer |
| Finished transformer | Core plus windings, tank and accessories | A transformer specification; outside the scope of a steel enquiry |
The rest of this checklist focuses on coil and slit coil, which is where most core makers buy, with notes on what changes when you also ask for cut laminations.
Grade and standard: name both
A grade name means little without the standard behind it. Common references for fully processed grain-oriented steel are IEC 60404-8-7, EN 10107 in Europe, ASTM A876 in the United States, JIS C 2553 in Japan and GB/T 2521.2 in China. Each sets its own designation, test conditions and tolerances.
In the EN 10107 system, for example, M105-30P means a maximum specific total loss of 1.05 W/kg at 1.7 T and 50 Hz, a nominal thickness of 0.30 mm, and P for the high-permeability type (S denotes the conventional type). Mill trade names often sit alongside these designations. Write the standard designation in the enquiry and add the trade name only as extra information.
If a supplier offers a grade from a different standard or a different mill, treat it as a substitution. Grades from different systems are tested and toleranced differently, so a similar-looking loss figure does not make them interchangeable. Any substitution needs review by your engineering team and, where the core goes into a customer design, approval from that customer.
Core loss and permeability: state the test condition
Core loss is the property most buyers care about and the one most often specified loosely. A figure such as 0.90 W/kg is meaningless unless it comes with the peak induction and frequency it applies to, usually written P1.7/50 for 1.7 T at 50 Hz. If your transformers run on 60 Hz networks or your designer works at 1.5 T, say so and ask whether the supplier can report values at that condition as well.
Also state the measurement method. Epstein frame testing under IEC 60404-2 and single sheet testing under IEC 60404-3 can give different numbers for the same steel, so the enquiry should say which method the guarantee and the certificate refer to. For high-permeability grades, ask for the magnetic polarization at 800 A/m (often written J800 or B8) as a second check.
Domain-refined grades need one more line. Some domain refinement, such as laser scribing, does not survive stress-relief annealing. If your cores are annealed after cutting, tell the supplier so they can confirm the offered grade is suitable for that route.
Thickness, width and coil format
Give the nominal thickness and the tolerance standard you accept. For slit coil, list every slit width with its tolerance, the maximum burr height, any camber limit and the edge condition you need. Add coil inner diameter, maximum outer diameter, coil weight range and whether you can handle eye-to-sky or eye-to-wall packing. These details decide whether the coil fits your decoiler and cut-to-length line without rework.
Worked example: a core maker needs three strips at 250 mm and two strips at 120 mm from a 1,000 mm master coil. The slit widths add up to 3 x 250 + 2 x 120 = 990 mm, which leaves 10 mm for edge trim. Whether 10 mm is enough depends on the master coil edge and the slitter, so the final layout should be confirmed by the processor before the order is placed.
Insulation coating and lamination factor
CRGO is normally supplied with an insulating coating on top of the base glass film. ASTM A976 classifies electrical steel coatings by composition and insulating ability, and surface insulation resistance can be measured under IEC 60404-11. If your process includes punching, welding, annealing or oil immersion, say so, because the coating has to tolerate it. If you need a minimum lamination (stacking) factor, measured under IEC 60404-13, state the value your core design assumes.
Processing and documents in a CRGO purchasing checklist
When you ask for processing, the enquiry becomes partly a drawing review. Send the lamination drawing with joint type, angles, lengths and holes, plus your burr limit and whether stress-relief annealing is part of the scope. MOOPEC accepts drawings through its technical drawing upload page so the processing route can be checked before a quote is issued.
For documents, name what you need rather than asking for “certificates”. A typical set is an inspection certificate type 3.1 under EN 10204 with the measured loss, polarization, thickness and coating data for each coil, a packing list that ties coil numbers to the certificate, and any material declarations your customers request. If you plan to buy remaining stock, accept it only when the coil identity, condition and documents are complete and traceable to the original certificate.
CRGO enquiry template
Copy this table into your RFQ and fill in every line. A blank line is a question the supplier will have to ask you later.
| Item | What to write | Example entry |
|---|---|---|
| Material form | Master coil, slit coil, laminations or core | Slit coil |
| Standard and grade | Standard designation; trade name optional | EN 10107 M105-30P |
| Thickness | Nominal thickness and tolerance basis | 0.30 mm, tolerance per EN 10107 |
| Width | Master width or each slit width with tolerance | 3 x 250 mm, 2 x 120 mm |
| Core loss | Maximum W/kg with induction, frequency and test method | 1.05 W/kg at 1.7 T, 50 Hz, Epstein |
| Permeability | Minimum polarization at 800 A/m, if required | State the value from your core design |
| Coating | Coating type and any process it must withstand | Standard insulating coating, suitable for stress-relief anneal |
| Lamination factor | Minimum value and method, if required | Per IEC 60404-13 |
| Slitting quality | Burr height, camber, edge condition | State your limits |
| Coil format | ID, maximum OD, weight range, packing orientation | 508 mm ID, eye-to-wall |
| Processing | Drawing, joint type, annealing scope | Drawing attached, step-lap, no anneal |
| Documents | Certificate type and data per coil | EN 10204 3.1 with measured loss per coil |
| Quantity and schedule | Total tonnage, call-offs, required date | Fill in for your order |
FAQ
Can I accept a different CRGO grade with a similar loss value?
Only after engineering review. Grades from different standards or mills are tested and toleranced differently, so a close loss figure is not proof of equivalence. Substitution needs approval from your engineering team and, where relevant, your customer.
Why does the test condition matter so much?
Core loss rises with induction and frequency, and Epstein and single sheet results can differ. A guarantee without induction, frequency and method cannot be checked against the certificate.
Should I buy master coil or slit coil?
Buy master coil if you have your own slitting line and need flexibility across many core sizes. Buy slit coil if you want strips ready for cutting, in which case the slit widths, burr and camber limits become part of the specification.
MOOPEC is a Singapore-headquartered industrial metals supplier with service centers in Shanghai and Wuhan, supplying CRGO electrical steel, slitting and lamination processing and transformer cores. Send your completed checklist through Tell Us What You Need, or upload a lamination drawing on the technical drawing page.
Cover photo by Michael Pointner on Pexels.